
Industrial Single-Tank & Special Cleaners
General-Purpose Heated Industrial Ultrasonic Cleaner
Versatile heated single-tank ultrasonic parts cleaner for general industry
View configuration
LENJEX Industrial Cleaning
Removes mold-release agent, oils, particles and processing residues from plastic and rubber parts with mild chemistry.
Why Ultrasonic
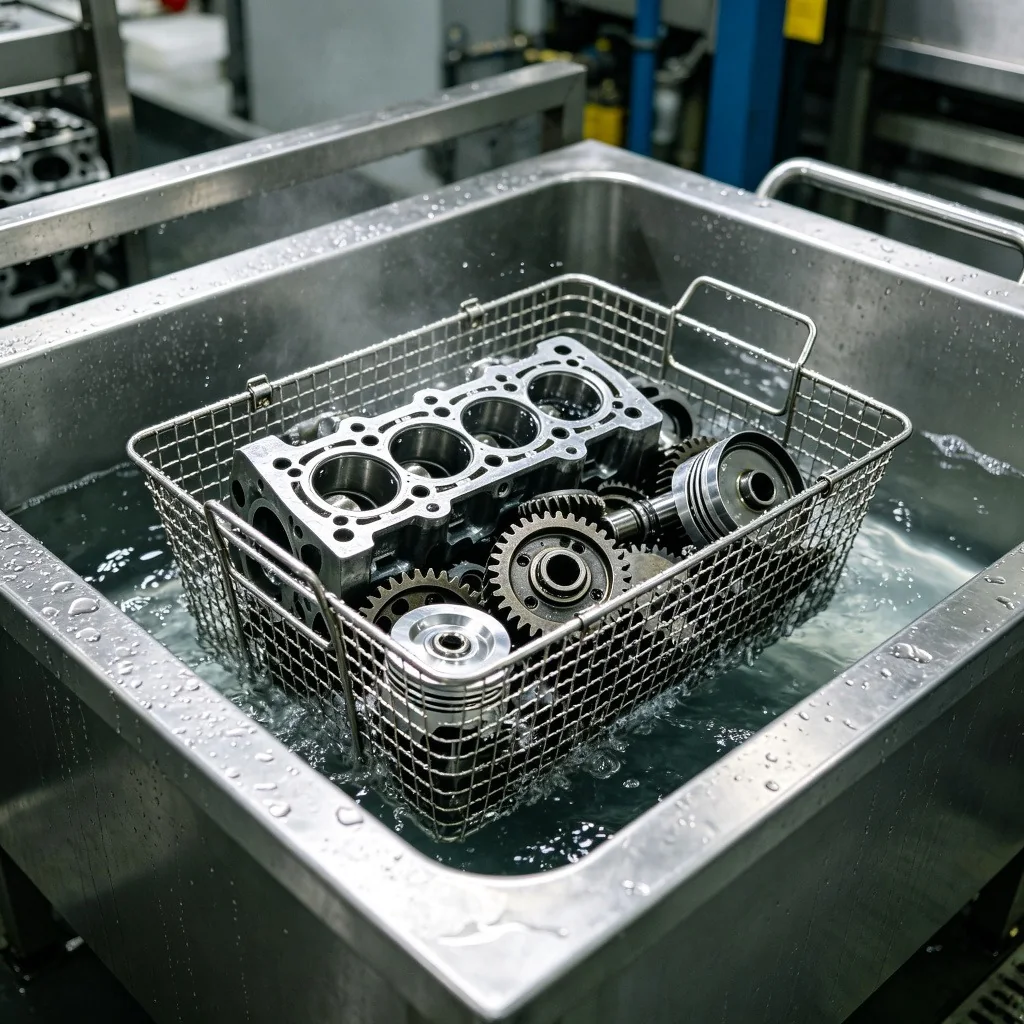
Plastic and rubber parts can retain mold-release agent, oils, particles and processing residues after molding. Gentle ultrasonic cleaning removes these surface contaminants without aggressive solvents that could stress, swell or mark the material.
A general-purpose heated cleaner or benchtop series uses mild, neutral chemistry. The work relates to water-based cleaning.
Temperature and chemistry must be validated against the specific plastic or rubber to avoid deformation or surface change.
Typical Workpieces
Contamination

Cleanliness Target
Acceptance is based on surface cleanliness and absence of release agent or residue before assembly, coating or bonding.
Temperature must stay below the point that affects the material.
Recommended Sequence
The final sequence depends on soil loading, material, rinse quality and drying behavior.
Recommended Equipment
The final specification follows process testing and production analysis.
Industrial Single-Tank & Special Cleaners
Versatile heated single-tank ultrasonic parts cleaner for general industry
View configuration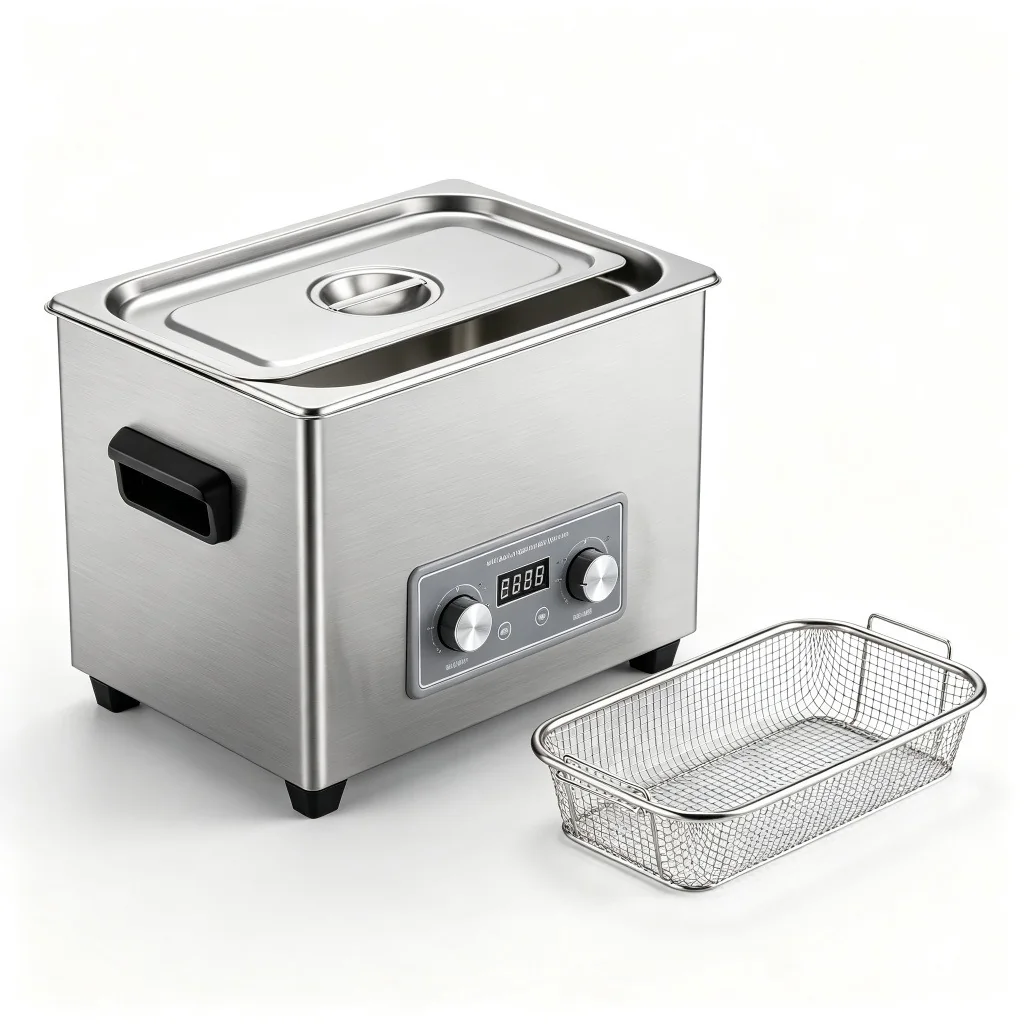
Benchtop & Laboratory Ultrasonic Cleaners
Small tabletop ultrasonic cleaners from 2 to 30 litres
View configuration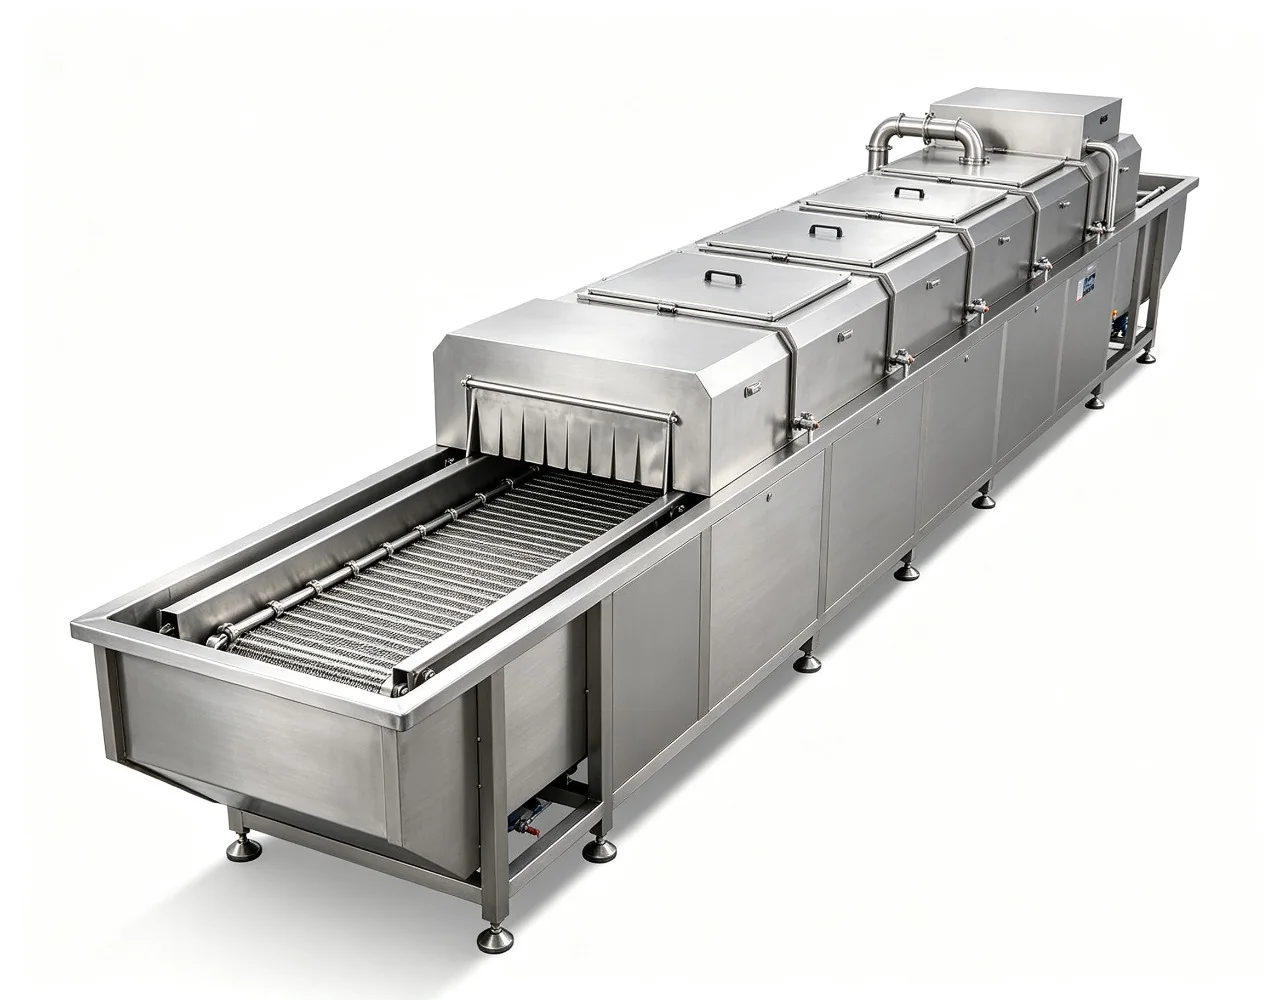
Multi-Tank & Automatic Cleaning Systems
Automatic rotating-basket multi-stage cleaning and drying line
View configurationProcess Controls
Confirm the part, soil, loading and final handling before fixing equipment settings.
Control 01
Record surfaces, cavities and features that can trap air or liquid.
Control 02
Test the heaviest representative contamination, not an ideal sample.
Control 03
Keep acoustic access and part spacing consistent with production.
Control 04
Match downstream handling to residue and corrosion risks.
System Selection
Stage count and automation follow the validated process and required output.
Batch
Compare for focused washing where rinsing and drying are managed separately.
Multi-stage
Add controlled stages when carryover and final condition matter.
Automatic
Evaluate automation when output, handling or recipe control requires it.
Acceptance
Use the same practical inspection method for trial samples and production parts.
Representative Trial
Trial evidence should cover normal production and the most difficult expected condition.
Application Questions
Include normal production parts and the most difficult expected geometry or contamination so the process is not based on an easy sample.
Provide part dimensions, material, soil, cleanliness target, parts per load, required output and available utilities.
It can if temperature or chemistry is unsuitable; these are validated with the specific material and kept within safe limits.
Yes, with mild chemistry and controlled temperature that remove release agent without swelling or damaging the rubber.
Mild, neutral water-based cleaners are typical for polymers, rather than aggressive solvents.
Related Applications
Industrial Application
Removes residual resin, support material, powder and processing media from printed parts, including lattice and internal structures.
View cleaning approach
Industrial Application
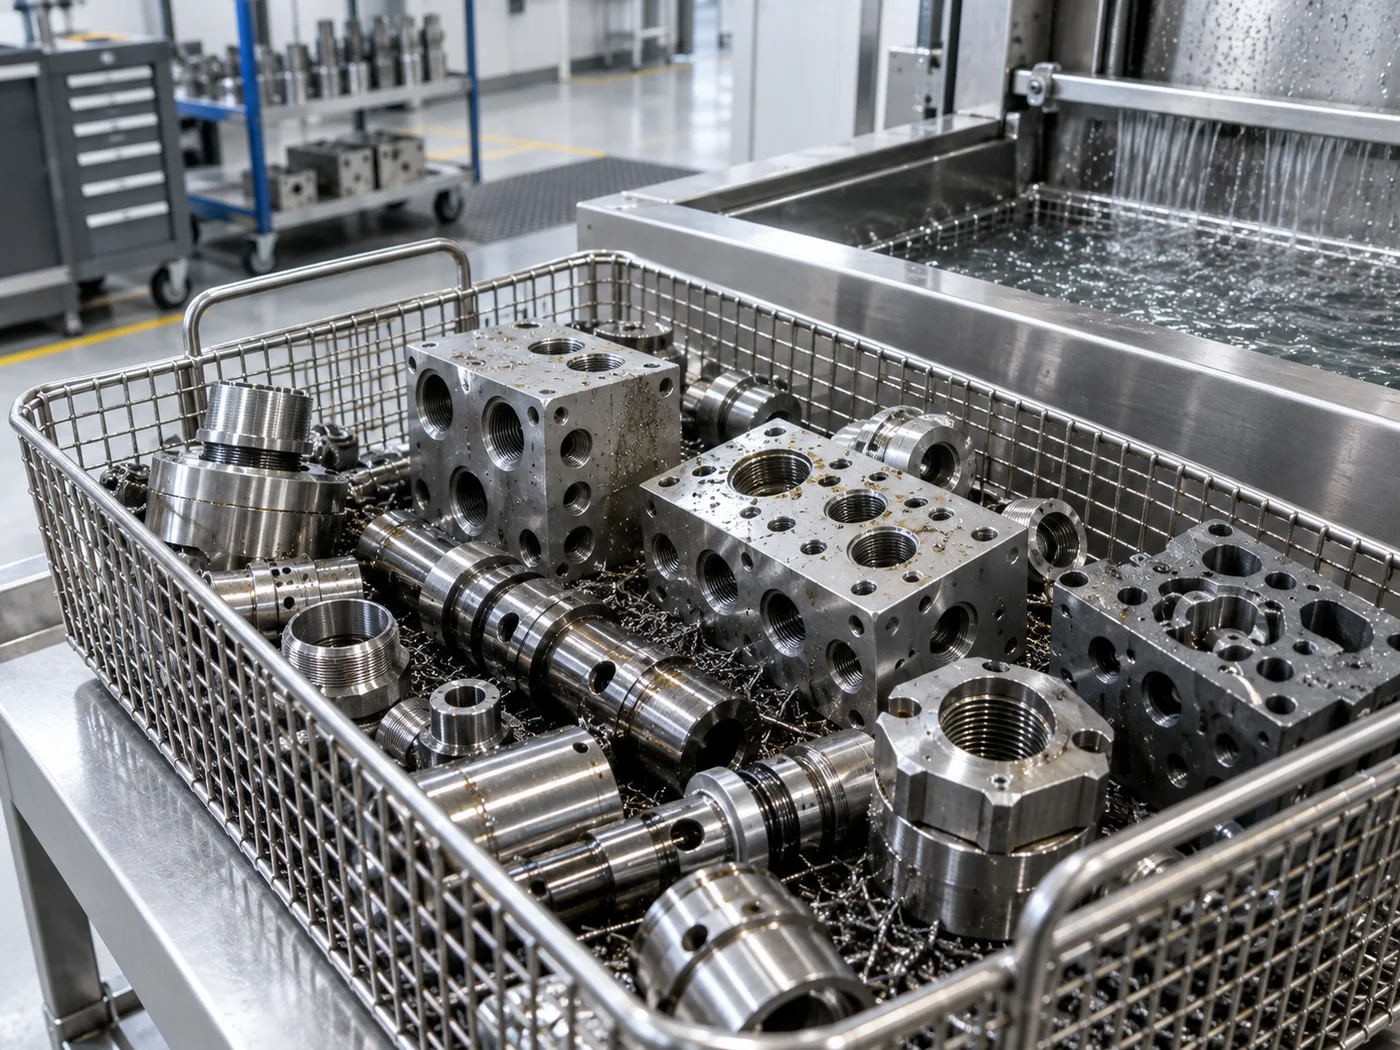
Metal parts vary widely in alloy, geometry, surface finish and soil load, so chemistry and energy must be selected as one process.
View cleaning approach
Industrial Application
Cleans glass components, vials, bottles and small containers, including interiors and narrow necks, without scratching.
View cleaning approach