
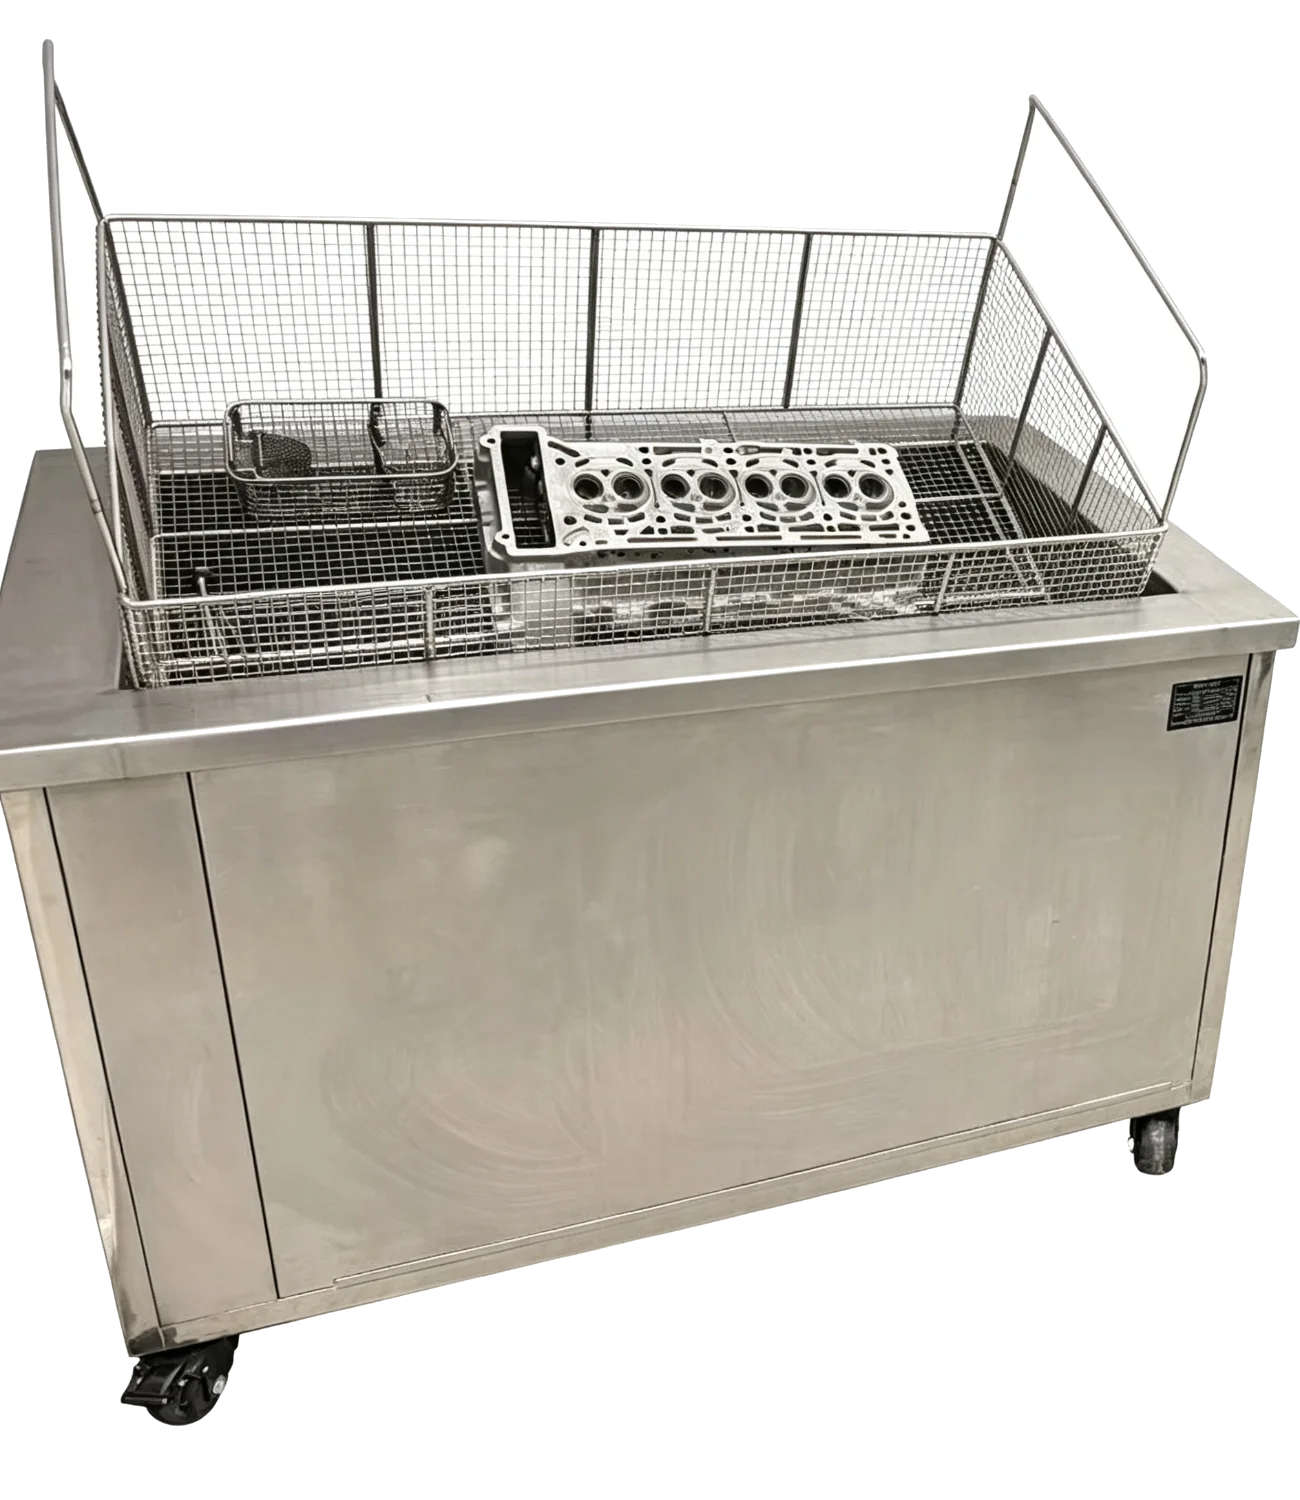
Single Tank Systems
Single-Tank Ultrasonic Cleaning Machine (Only Cleaning / Cleaning with Filtration)
Two configurations: ultrasonic cleaning only, or ultrasonic cleaning with circulating filtration and oil-water separation.
View configuration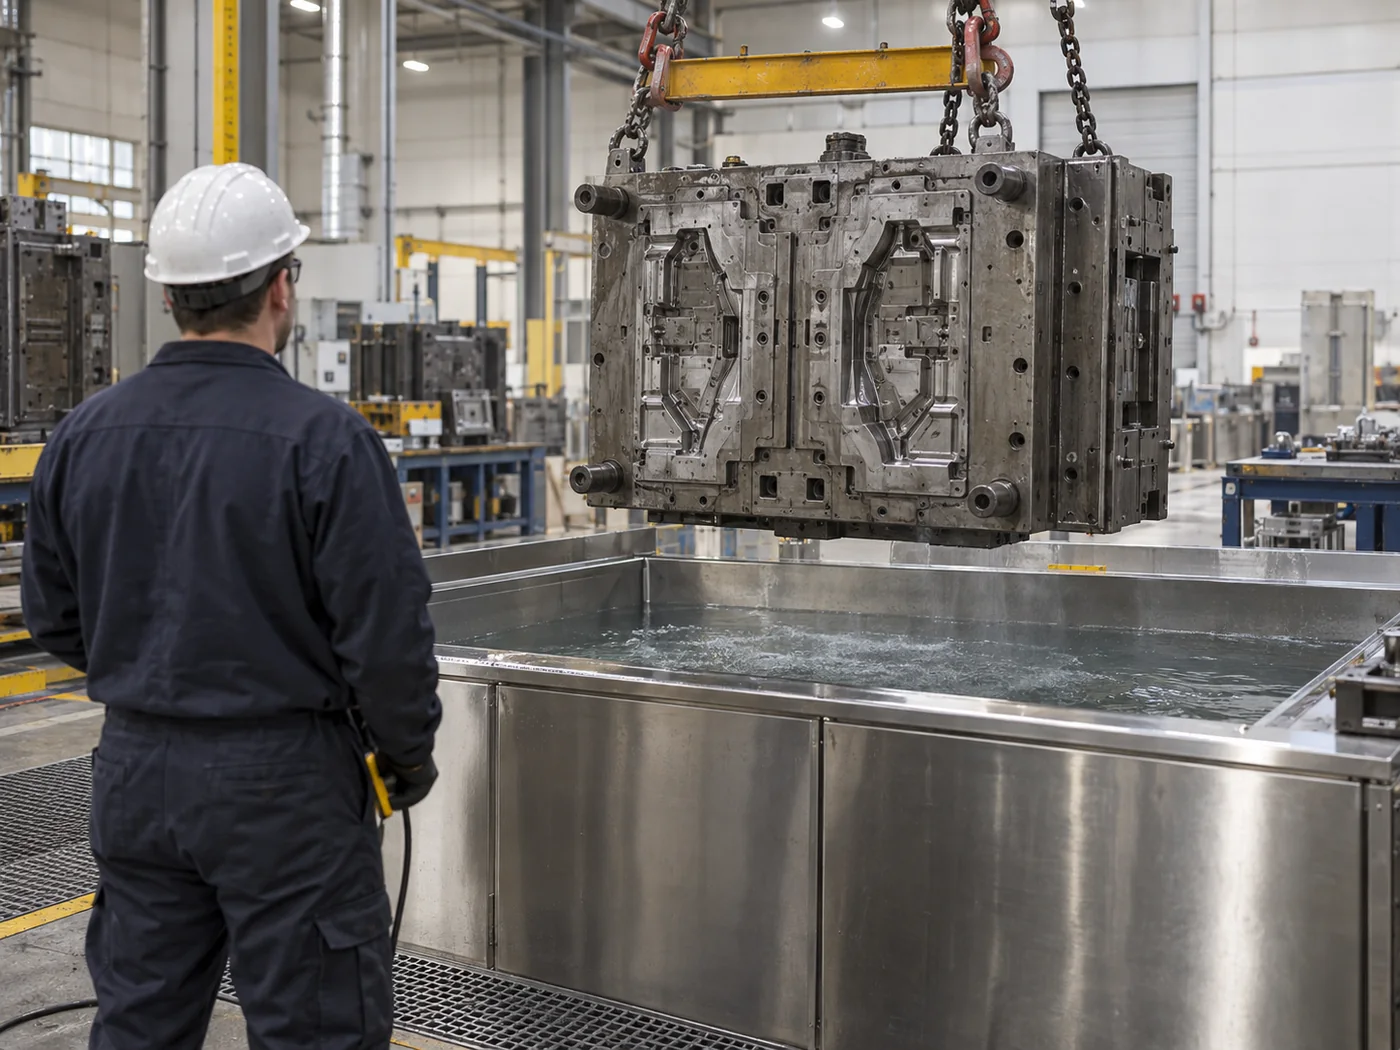
LENJEX Industrial Cleaning
Molds combine heavy mass, complex cavities and surface-finish requirements. Cleaning must reach detail without damaging working surfaces.
Typical Workpieces
Contamination
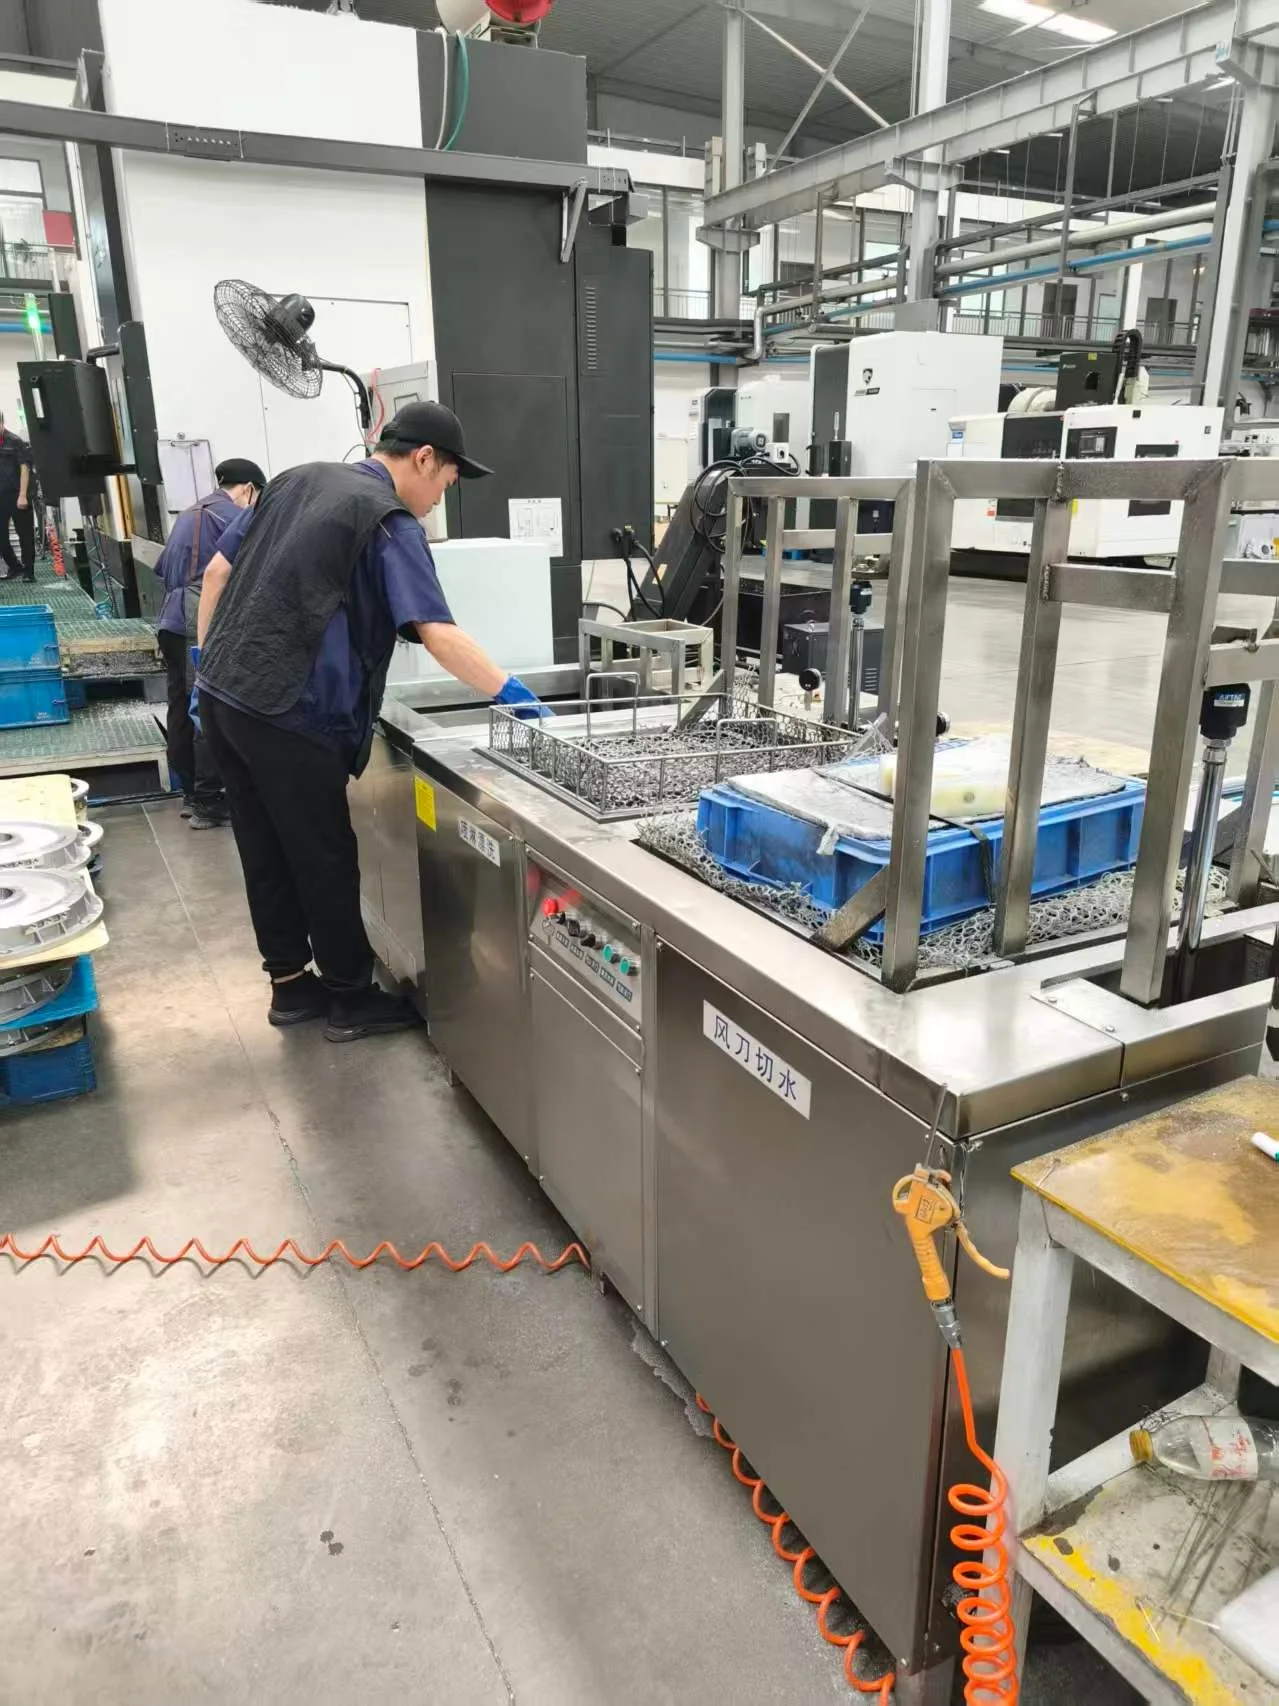
Cleanliness Target
The target is a residue-free working surface with controlled handling for heavy tools and minimal manual scraping.
The acceptance method should be practical for trials and production, with agreed sample handling and inspection timing.
Recommended Sequence
The final sequence depends on soil loading, part material, rinse quality and drying behavior.
Recommended Equipment
These equipment families support the application review; the final specification follows process testing and production analysis.
Single Tank Systems
Two configurations: ultrasonic cleaning only, or ultrasonic cleaning with circulating filtration and oil-water separation.
View configuration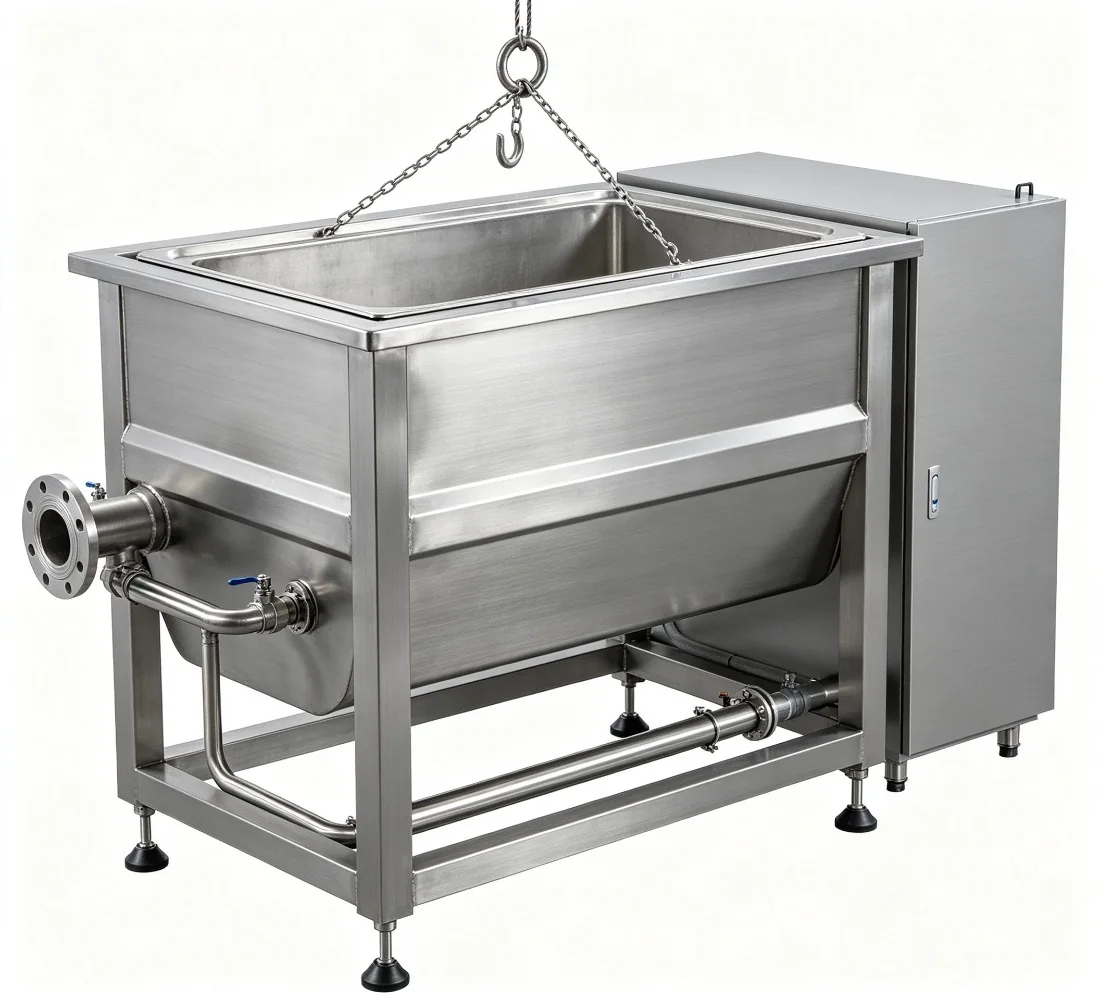
Single Tank Systems
A reinforced 960-3744 L ultrasonic bath with multi-face transducers and independent power zones for oversized, heavy or heavily soiled parts.
View configuration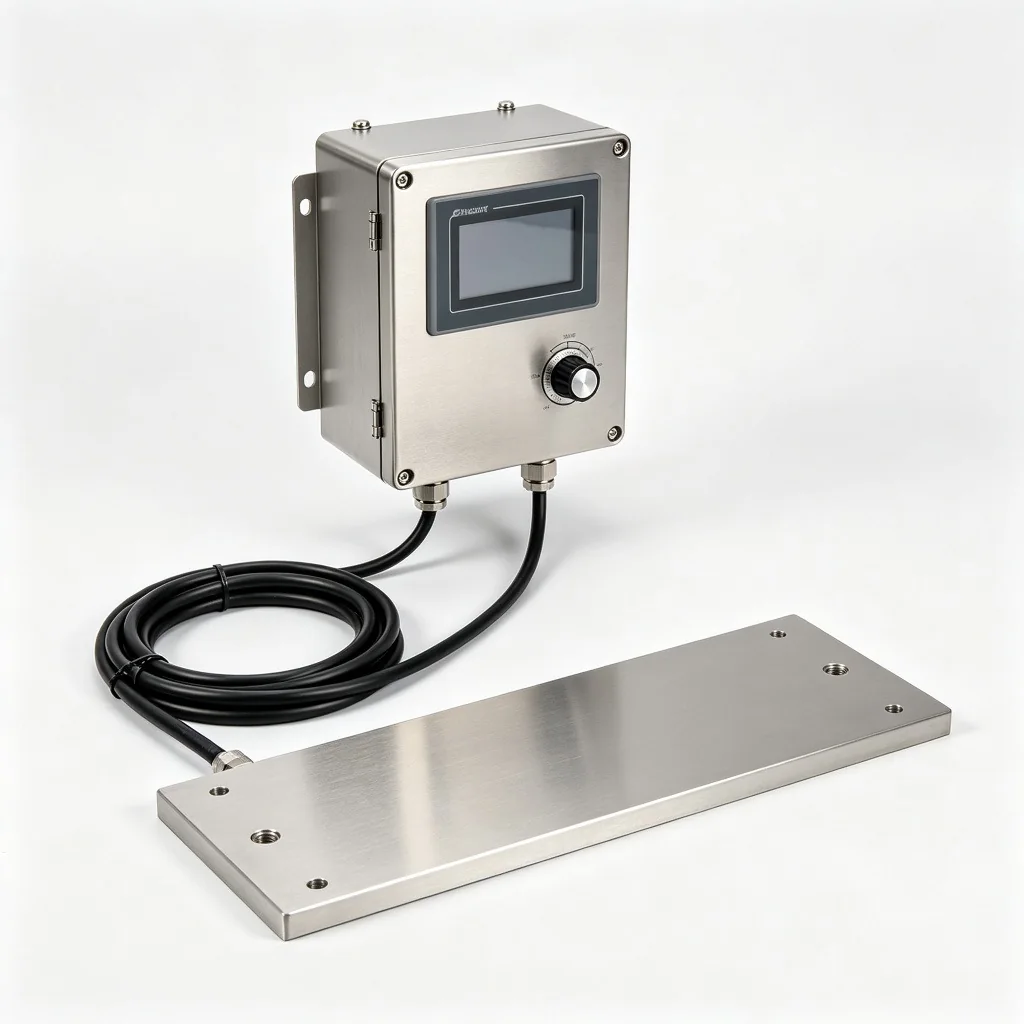
Ultrasonic Components
A sealed 600-1200 W stainless transducer module for adding ultrasonic power to existing tanks, custom vessels and multi-stage systems.
View configurationProcess Controls
Confirm the part, soil, loading and final handling before fixing equipment settings.
Control 01
Record surfaces, cavities and features that can trap air or liquid.
Control 02
Test the heaviest representative contamination, not an ideal sample.
Control 03
Keep acoustic access and part spacing consistent with production.
Control 04
Match downstream handling to residue and corrosion risks.
System Selection
Stage count and automation follow the validated process and required output.
Batch
Compare for focused washing where rinsing and drying are managed separately.
Multi-stage
Add controlled stages when carryover and final condition matter.
Automatic
Evaluate automation when output, handling or recipe control requires it.
Acceptance
Use the same practical inspection method for trial samples and production parts.
Representative Trial
Trial evidence should cover normal production and the most difficult expected condition.
Application Questions
Include normal production parts and the most difficult expected geometry or contamination so the process is not based on an easy sample.
Provide part dimensions, material, soil, cleanliness target, parts per load, required output and available utilities.
Use representative materials, geometry, contamination and load density. Evaluate the cleaned surface with the same acceptance method used in production.
Tank volume, frequency, filtration, rinse stages, drying and transfer are selected after the workpiece, soil, cleanliness and throughput are defined.
A validated batch or multi-stage process can provide the basis for gantry, robotic or conveyor automation when production demand supports it.